A rental can solve a breakdown repair, shutdown, trial run, overflow job or one-off site weld only when the machine, gas, power supply and consumables arrive as one workable system. By checking the process requirements, site conditions, hire terms and acceptance tests, you can determine whether a short rental will reduce downtime or create an avoidable setup failure.
Key takeaways
- Rent for breakdowns, shutdowns and uncertain workloads instead of buying rarely used equipment.
- Demand a complete package: power source, wire feeder, torch, regulator, cables and earth clamp.
- Size the machine for wire diameter, duty cycle, supply power and site access.
- Record a pre-weld inspection, test gas flow and confirm hire support before welding.
When does a short-term CO2/MAG rental make practical sense?
Rental services for co2 mag welding make practical sense when the job is short, urgent or too uncertain to justify another machine. A breakdown repair can restore production faster than purchasing equipment; a planned shutdown can avoid leaving a rarely used asset on the books.
Trial production, overflow fabrication and a one-off site assignment also suit hire when mobilisation is quick and a qualified operator is available.
| Option | Best fit | Main decision |
|---|---|---|
| Hire a complete package | Breakdown, shutdown, trial, overflow or one-off site work | Arc-on time is limited and rapid mobilisation costs less than idle production |
| Use existing equipment | Routine work with an available qualified operator | Setup and process qualification already match the job |
| Buy equipment | Repeated work with high arc-on time | Cumulative hire charges and downtime risk exceed ownership cost |
| Subcontract the work | No qualified operator, procedure or suitable site power | A fabricator can provide controlled production and inspection |
| Hire a partial package | You already have compatible feeder, torch, gas control and cables | Missing components will otherwise delay welding |
Calculate expected arc-on time, not the shift length. Long welds, high deposition rates or mechanised work can overheat a nominally adequate unit, while tacking and repositioning reduce demand. Confirm material, thickness, wire, gas, power and duty cycle before booking.
For structural work, hiring equipment does not replace a qualified welding procedure, qualified operators, traceable consumables or inspection records. If the process is not qualified, subcontracting is safer than treating rental as a shortcut.
What must be included in a production-ready MAG package?
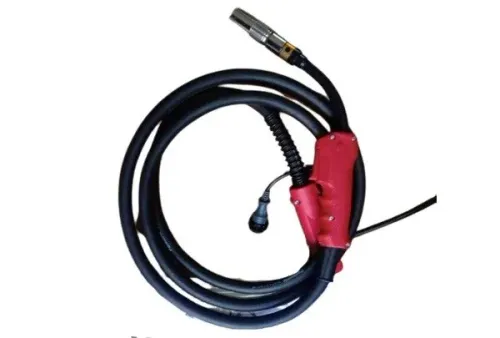
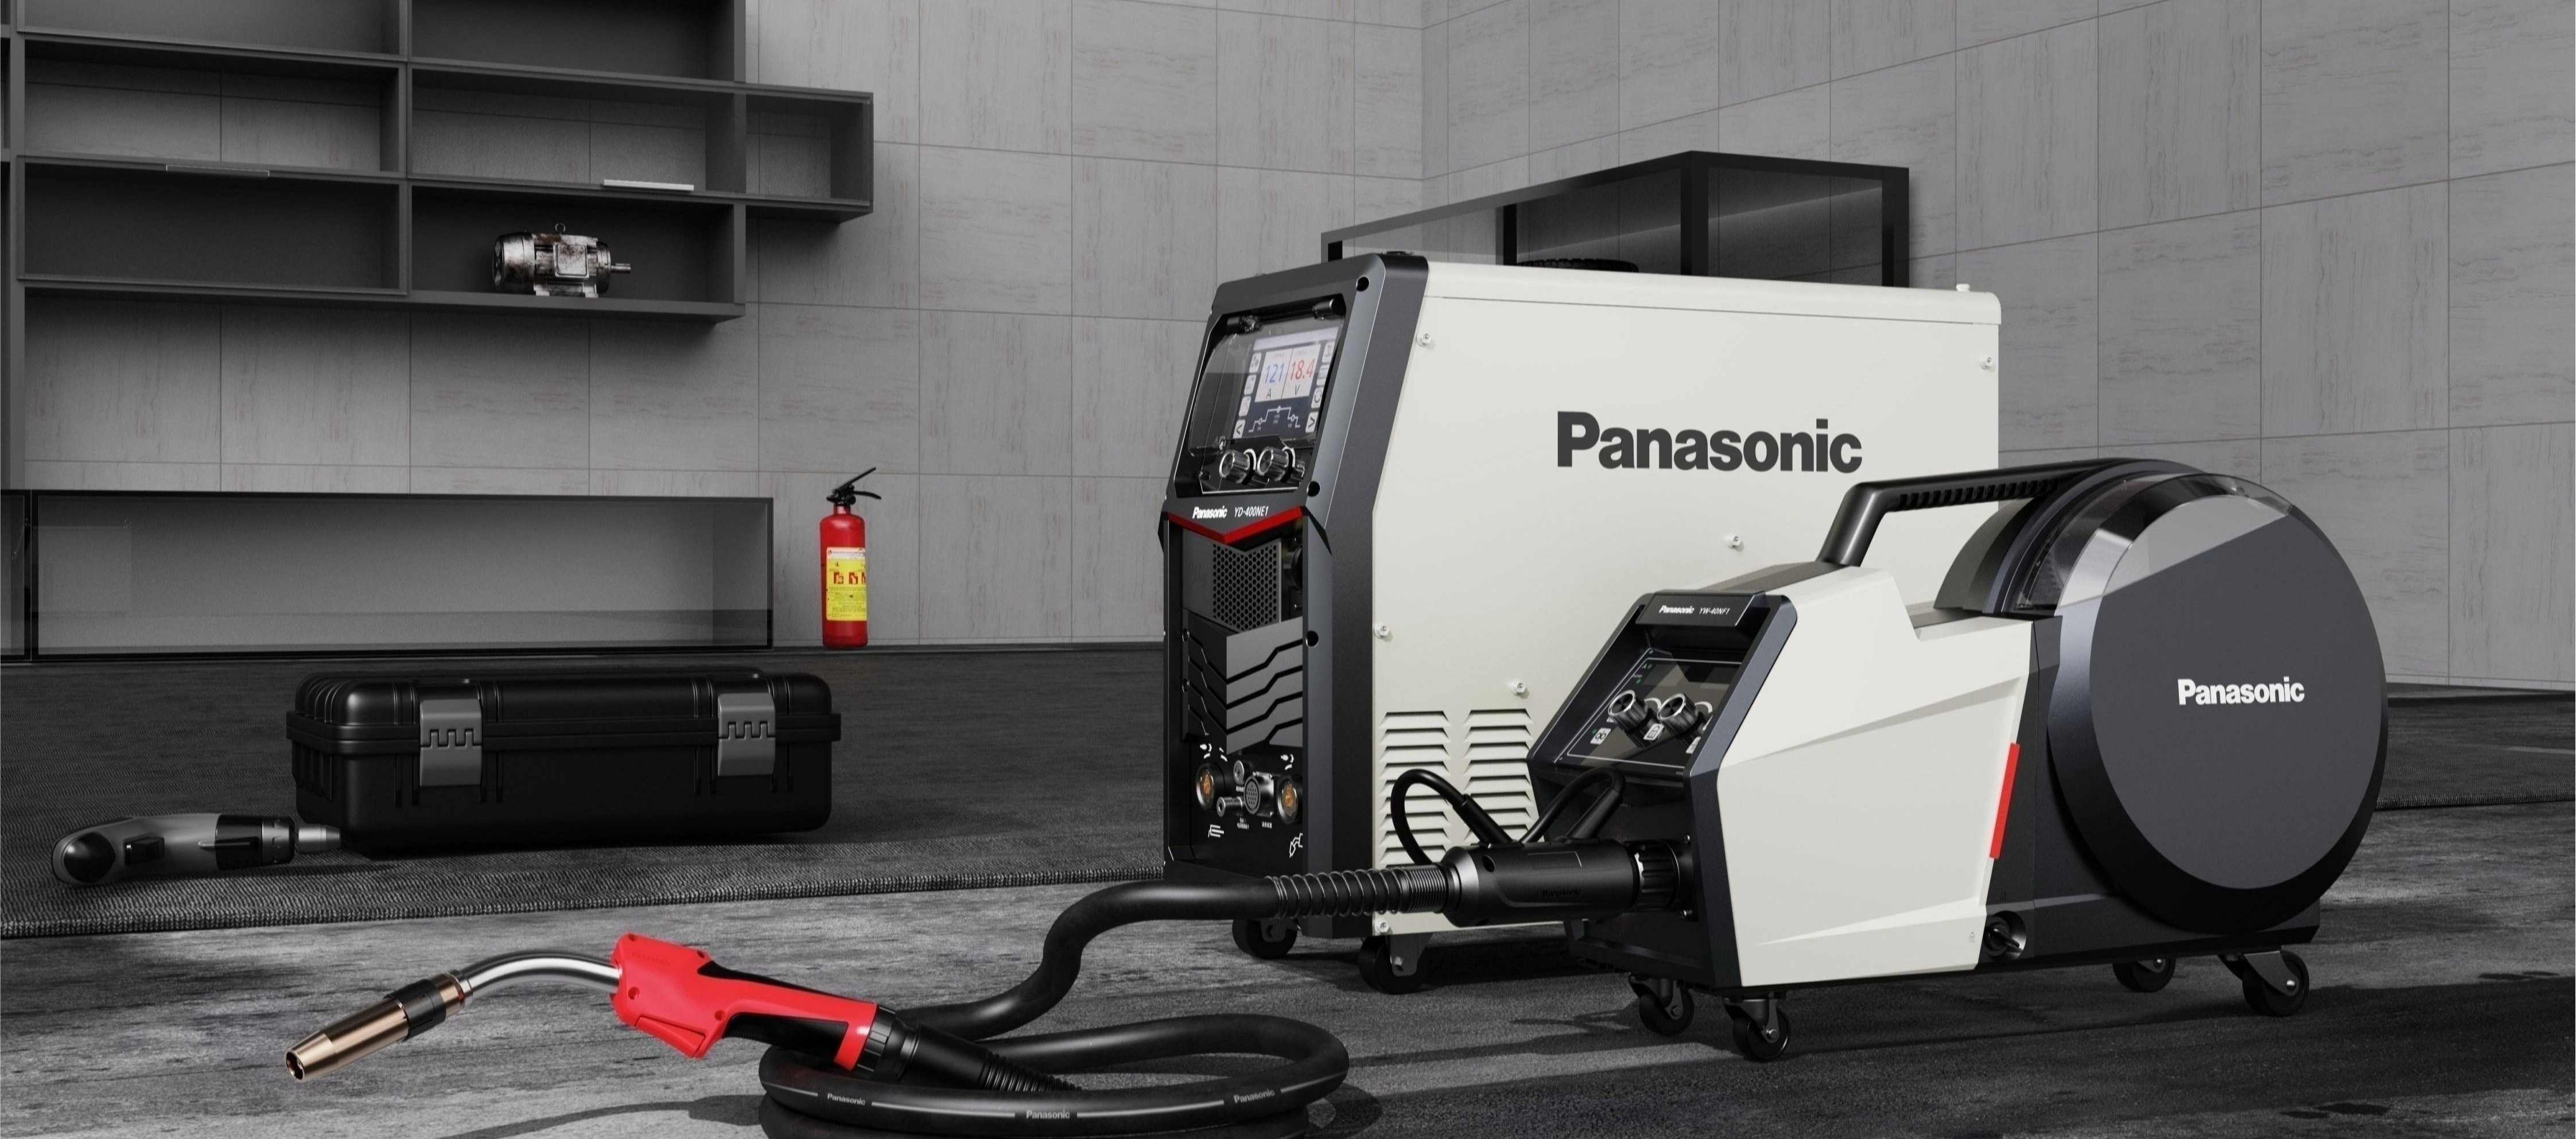
A production-ready package includes a constant-voltage power source, wire feeder, compatible torch, work-return lead, regulator and flowmeter, gas cylinder or bulk-gas connection, and trolley. It also includes the consumables that make the system feed reliably: drive rolls, liner, contact tips and nozzles.
| Option | What you receive | When it applies |
|---|---|---|
| Complete MAG package | Power source, feeder, torch, return lead, gas controls, trolley and matched consumables | You need to start welding immediately at a temporary site |
| Power-source-only hire | Constant-voltage machine without the complete feeding and gas system | You already own a compatible feeder, torch and accessories |
| Torch or spare-parts hire | Torch, liner, tips, nozzles or drive components | Your existing set has a failed or worn part |
For solid-wire MAG, specify DCEP, wire diameter and classification, drive-roll profile, liner bore, contact-tip size and feed-roll pressure together. Steel solid wire commonly uses V-groove rolls and a steel liner; a worn liner or incorrect roll causes feed slip, bird-nesting and burnback.
State the exact shielding gas in the quotation. Pure CO2 is an active MAG gas: it gives deeper, harsher penetration and more spatter, while argon–CO2 mixtures produce a smoother arc, cleaner finish and less nozzle cleaning.
Argon-rich blends support spray transfer when current and wire size are suitable; pure CO2 is not a substitute for that procedure. Gas cost and availability also change.
For short term co2 welding equipment, confirm gas quantity, torch length, consumable quantities and the intended transfer mode, not just the machine’s amperage. A power source that functions electrically is not automatically a production-ready package.
How do you size the rental machine for the work and site?
A 350 A machine is suitable only when its process output and site supply match the job. For mag welding machine hire, specify the material grade and thickness, wire diameter and classification, shielding gas, target current and voltage, polarity, stick-out and transfer mode before accepting the quotation.
1. Match the process: confirm that the proposed machine supports the required short-circuit, globular or spray transfer range. Wire-feed speed, voltage, gas composition, stick-out and thickness work together; an argon-rich mixture is normally needed for spray transfer, while pure CO2 is not a drop-in substitute.
2. Calculate heat demand from actual arc-on time, not an eight-hour shift. Tacking, repositioning and wire changes reduce it; long welds, high deposition rates and mechanised welding increase it. A 60% duty cycle means six minutes of welding followed by four minutes of cooling within every 10-minute period, at the manufacturer’s stated output.
3. Check the site before dispatch. Record whether 380–415 V three-phase power is available, the phase arrangement, breaker rating, earthing, plug type and cable length. Long leads can cause voltage drop, nuisance trips and unstable wire feeding; confirm generator compatibility and rated capacity.
4. Inspect access and the work area: measure doorways and route distances, provide wind protection for shielding gas, and confirm fume extraction and fire controls. State the required torch length, consumable quantities and return location so a technically capable machine does not arrive unusable.
Which hire terms prevent a technically correct machine from failing on site?
Do not accept industrial welding rental options until the quotation defines responsibility for the machine and the job. State the minimum hire duration, extension rate and notice period, delivery, transport, installation, commissioning, operator instruction, pickup, security deposit, downtime credit, late-return charge, repair cost and damage liability.
| Quotation item | Confirm before acceptance | Failure prevented |
|---|---|---|
| Site service | Delivery date, installation, commissioning and breakdown response time | A usable machine sitting idle |
| Hire control | Minimum term, extension, pickup, transport and late-return rules | Surprise charges after the job |
| Risk allocation | Deposit, repair costs, damage liability and downtime treatment | Disputes over faults or delays |
| Consumables | Wire diameter and classification, gas composition and quantity, cylinder rental or exchange | Running out of wire or shielding gas |
Ask separately whether contact tips, nozzles, liner and torch servicing are included. A cylinder that lasts less than the planned arc-on time can stop production even when the power source works.
For a Pune buyer, Weld Tech Corporation can help compare a complete package with individual Panasonic-compatible equipment, but you must supply the selection data:
- Material and thickness
- Wire, gas composition and target power
- Expected arc-on time and site environment
- Return condition, including consumable wear and damage reporting
A complete package reduces coordination; itemised hire can avoid paying for equipment you already own. Confirm that the quotation covers fume and fire controls where the worksite requires them. Rental services for co2 mag welding fail commercially when these details remain verbal.
Related products
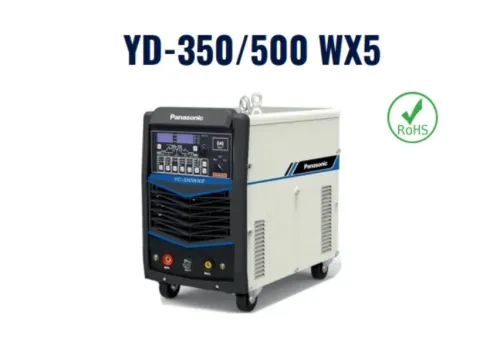
 | CO2 welding machine Inverter IGBT-Controlled CO2/MAG Welding Machine Advanced arc stability for high-quality welds Flexible parameter settings for materials & thicknesses Robust build for long-term durability in... View product → |
 | MIG Welding Machines Digital + Inverter IGBT-Controlled MIG/MAG Welding Machine Available in 250 AMP, 400 AMP & 500 AMP options Energy Saving & High Reliability Soft Arc (Thin Metal) & Hard Arc (Thick Metal) Characterisitcs... View product → |
How should you inspect and control a hired MAG set before welding?
Accept the short-term CO2 welding equipment only after you document its identity, condition and operating proof. Photograph the serial number, hour or meter readings, control panel and accessories before connection, then record dents, missing covers, damaged plugs, contamination and the agreed return condition.
- Inspect the output leads, Euro connection, torch liner, contact tip, nozzle, wire-feed rollers, gas solenoid, display, cooling fan, earth clamp and cable insulation. Reject loose connections, crushed liners, worn rollers, cracked insulation or a clamp that cannot bite clean metal.
- Fit the specified wire and gas, then confirm gas flow at the torch, correct polarity, stable wire feeding, reliable arc start and work-return continuity. Make a test weld on representative material; check arc sound, penetration, porosity, spatter and wire burn-back before signing the handover.
- Record nozzle condition and agree nozzle-cleaning intervals, anti-spatter use and replacement quantities. Excessive flow wastes gas and can draw air into the shield; insufficient flow causes porosity.
- Confirm fume extraction, general ventilation and fire controls before welding. CO2 can displace oxygen in pits, tanks and poorly ventilated rooms, so measure the atmosphere and apply confined-space controls where required.
- Confirm the operator’s qualification, welding procedure, traceable wire and gas, and inspection records. For welds affecting structural integrity, MAG welding machine hire supplies equipment, not an acceptable qualification system; follow the governing fabrication code and stop if those controls are absent.
Frequently asked questions
When does short-term CO2/MAG welding rental make practical sense?
Use rental services for CO2/MAG welding for breakdown recovery, planned shutdowns, short contracts, overflow production or work where future demand is uncertain.
What must be included in a production-ready MAG rental package?
Confirm that the package includes the power source, wire feeder, MIG/MAG torch, earth clamp and lead, work cable, gas regulator and flowmeter, welding wire and compatible spare contact tips.
How do you size a rental MAG welding machine?
Match output current and duty cycle to the wire diameter, material thickness and weld length, then verify the site supply voltage, phase, outlet rating, cable length and machine access route.
Which hire terms prevent a technically correct machine from failing on site?
Specify delivery and collection dates, included accessories and consumables, replacement arrangements, breakdown response, operator support, damage responsibility and testing records before accepting the set.
How should you inspect and control a hired MAG set before welding?
Check cables, connectors, torch liner, contact tip, earth clamp, wire feed, gas hose, regulator and machine controls; confirm gas flow, polarity and a test weld before production.
Related product
 | MAG Welding Machines Panasonic MAG Welding Machines Brand Panasonic Model YD-350GZ4 Phase 3-Phase Current 350 A Voltage 380-415 V Dimension (L x B x H) 380x550x640 mm Product Type New Duty Cycle 60%... View product → |